Industrial safety depends on one critical principle: pressure must never be allowed to exceed the safe operating limits of a system. Whether it’s a boiler, a chemical reactor, or a pipeline carrying high-pressure gas, uncontrolled pressure buildup can lead to catastrophic failure, equipment damage, and serious safety hazards. This is where direct acting pressure relief valves come in — simple, reliable, and fast-responding devices designed to protect systems the moment pressure crosses a set threshold.
As industries across India continue to expand in sectors like oil & gas, power generation, chemical processing, and water treatment, the demand for dependable safety valve solutions has grown significantly. Choosing the right Pressure Relief Valve Manufacturer is no longer just a procurement decision — it’s a safety-critical one. In this guide, we’ll break down what direct acting pressure relief valves are, how they work, their key applications, and why partnering with an experienced Indian manufacturer like Micado Valves makes all the difference.
What Is a Direct Acting Pressure Relief Valve?
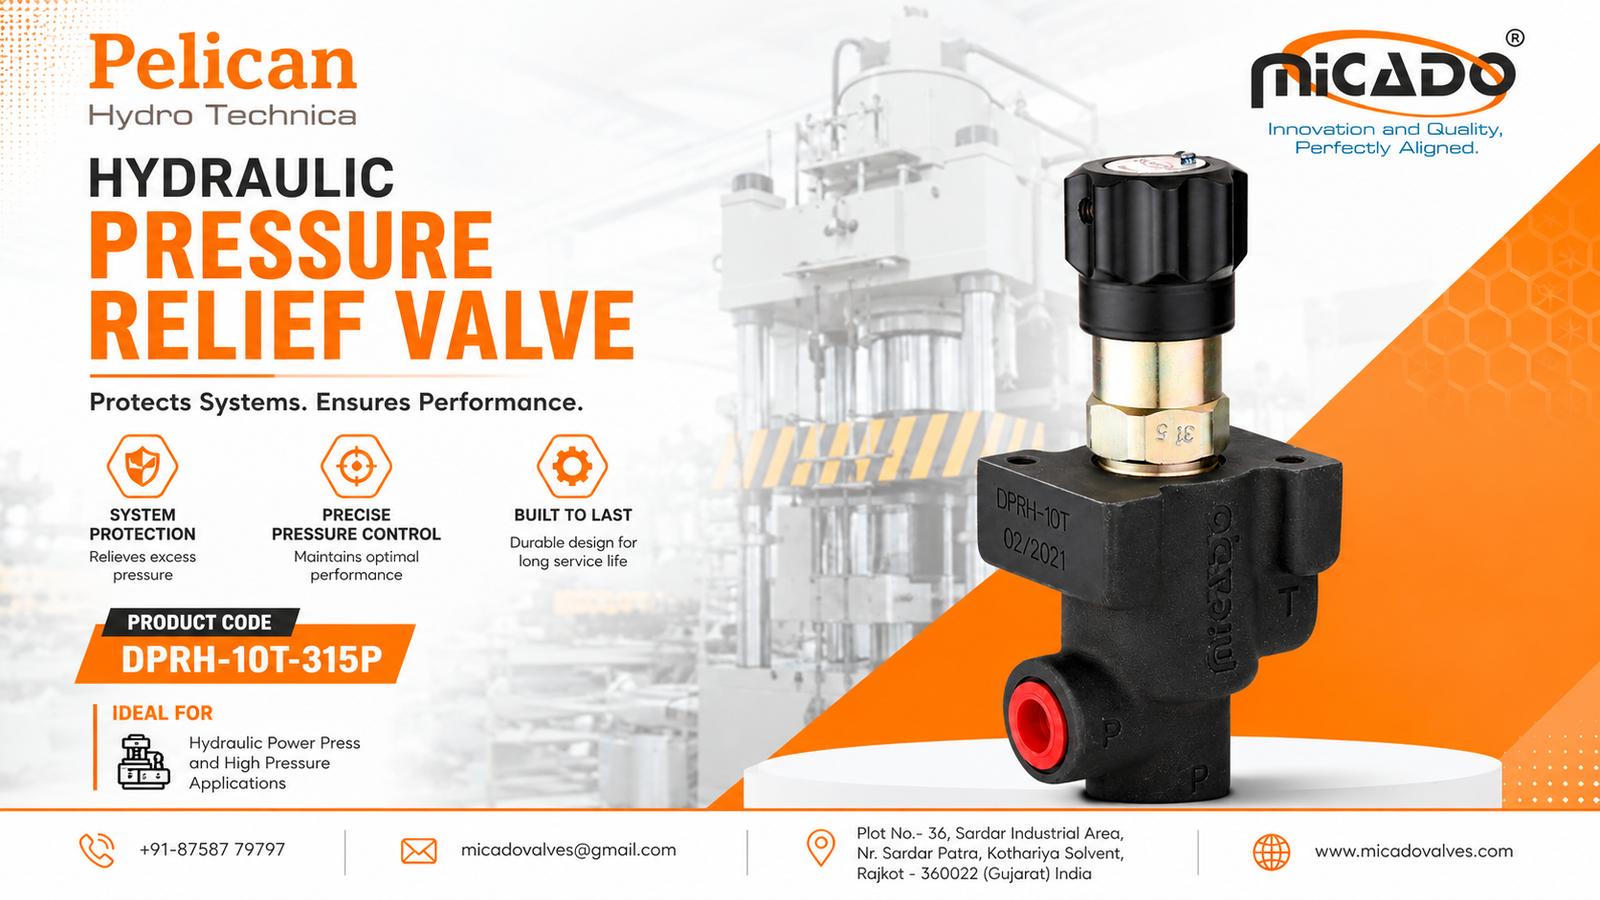
A direct acting pressure relief valve is a self-actuated safety device that uses a spring mechanism to hold a disc or poppet against a valve seat. When system pressure exceeds the spring’s preset force, the valve opens automatically, releasing excess pressure until the system returns to a safe operating range — at which point the valve reseats itself.
Unlike pilot-operated relief valves, which rely on an external pilot system to sense pressure and trigger the main valve, direct acting valves respond immediately and mechanically to pressure changes at the inlet. This makes them simpler in design, faster in response time, and easier to maintain — qualities that make them a preferred choice for a wide range of industrial applications where reliability and quick response matter most.
How Direct Acting Relief Valves Work
The operating principle is straightforward:
- Normal operation – The valve remains closed, with the spring force balancing the system pressure against the disc.
- Overpressure event – As pressure rises above the set point, it overcomes the spring force, lifting the disc off its seat.
- Relief phase – Excess fluid or gas is released through the valve outlet, reducing system pressure.
- Reseating – Once pressure drops back to a safe level, the spring pushes the disc back onto the seat, closing the valve.
This mechanical simplicity is precisely why direct acting valves are trusted across so many industries — fewer components mean fewer points of failure, and that translates directly into safer operations.
Why Choose an Experienced Pressure Relief Valve Manufacturer in India
India has emerged as a major hub for industrial valve manufacturing, combining strong engineering capabilities with cost-competitive production. Working with a reputable Pressure Relief Valve Manufacturer based in India offers several strategic advantages for both domestic and international buyers:
- Quality engineering at competitive costs – Indian manufacturers combine skilled labor, modern manufacturing infrastructure, and quality raw materials to deliver valves that meet international performance standards without the premium pricing of Western suppliers.
- Customization capabilities – A knowledgeable manufacturer can tailor set pressures, materials, end connections, and accessories to match exact process requirements rather than forcing a one-size-fits-all solution.
- Faster lead times for regional buyers – Sourcing locally or regionally reduces shipping delays, simplifies logistics, and supports quicker turnaround on urgent replacement orders.
- Strong compliance track record – Established Indian manufacturers design and test valves in line with recognized standards such as API, ASME, and IS specifications, ensuring the equipment performs reliably under real-world conditions.
- Responsive technical support – Proximity matters when you need design consultation, installation guidance, or after-sales service for a safety-critical component.
This combination of quality, customization, and service is exactly why companies across the globe increasingly look to a trusted Pressure Relief Valve Manufacturer in India rather than relying solely on distant suppliers.
Products Offered by Leading Direct Acting Valve Manufacturers
A comprehensive Pressure Relief Valve Manufacturer typically offers a range of direct acting valve configurations designed for different media, pressures, and industry requirements, including:
- Spring-loaded pressure relief valves – The most common type, used across a broad range of pressure and temperature conditions.
- Safety relief valves for steam, air, and gas systems – Designed to handle compressible fluids with rapid pressure changes.
- Liquid relief valves – Engineered specifically for hydraulic and liquid-filled systems where response characteristics differ from gas applications.
- Bellows-sealed relief valves – Ideal for applications where backpressure could otherwise affect valve performance.
- Corrosion-resistant valve variants – Manufactured from stainless steel, alloy steel, or specialty materials for use in aggressive chemical environments.
Each of these products is typically available in multiple sizes, pressure ratings, and end connection types (flanged, threaded, socket-weld, or butt-weld), allowing engineers to specify exactly what their system requires.
Key Applications of Direct Acting Pressure Relief Valves
The versatility of direct acting relief valves means they’re deployed across nearly every major industrial sector:
Oil & Gas Industry
Protecting pipelines, storage tanks, and processing equipment from pressure surges that could otherwise lead to leaks, ruptures, or fires.
Power Generation
Safeguarding boilers, steam systems, and turbines, where sudden pressure spikes can compromise both equipment integrity and personnel safety.
Chemical & Petrochemical Processing
Managing pressure in reactors, storage vessels, and piping systems that handle volatile or hazardous substances.
Water & Wastewater Treatment
Regulating pressure in pumping stations and distribution networks to prevent pipe bursts and equipment strain.
Pharmaceutical & Food Processing
Ensuring pressure vessels used in sterilization, mixing, and processing stay within safe operational limits.
HVAC & Compressed Air Systems
Protecting compressors and air receivers from overpressure damage in industrial and commercial settings.
Because these industries operate under strict safety regulations, sourcing from a certified Pressure Relief Valve Manufacturer is essential to ensure compliance and long-term operational reliability.
Benefits of Direct Acting Pressure Relief Valves
Direct acting valves continue to be a preferred choice for engineers and procurement teams because they offer several practical benefits:
- Fast response time – Direct mechanical actuation means there’s no delay waiting for a pilot signal, which is critical during rapid pressure surges.
- Simple design, easy maintenance – Fewer moving parts translate into lower maintenance costs and easier troubleshooting over the valve’s service life.
- Reliable performance in remote or harsh environments – Since they don’t depend on external power or pilot systems, they continue functioning even in installations where auxiliary systems might fail.
- Cost-effective safety solution – Lower manufacturing complexity generally makes direct acting valves more affordable than pilot-operated alternatives, without compromising core safety performance.
- Wide compatibility – Suitable for a broad range of pressures, temperatures, and media types across multiple industries.
Choosing the Right Manufacturer for Your Project
When evaluating a Pressure Relief Valve Manufacturer, buyers should look beyond price alone. Key factors to assess include manufacturing certifications, material traceability, testing protocols, customization flexibility, and the manufacturer’s track record in your specific industry. A manufacturer with in-house engineering support can also help you select the correct set pressure, orifice size, and materials for your exact application — reducing the risk of costly oversizing or undersizing.
Companies like Micado Valves have built their reputation on combining engineering expertise with rigorous quality control, offering direct acting pressure relief valves that meet the demanding safety requirements of modern industrial operations.
Conclusion
Direct acting pressure relief valves remain one of the most trusted safety solutions across industrial sectors, thanks to their simplicity, speed, and reliability. As demand for high-quality, cost-effective safety equipment continues to grow, partnering with an experienced Pressure Relief Valve Manufacturer in India gives businesses access to world-class engineering, competitive pricing, and responsive technical support — all essential ingredients for maintaining safe and efficient industrial operations.
If you’re evaluating suppliers for your next project, prioritize manufacturers with proven compliance standards, customization capabilities, and a strong service track record to ensure your systems stay protected for years to come.