Every hydraulic system needs to hold a load safely. It must do this without drift. The component doing this work is a check valve — but not just any check valve. Applications where an actuator must stay locked under pressure need a pilot operated check valve. Nothing else does the job reliably.
Finding the right Pilot Operated Check Valve Manufacturer is not a small decision.
At Micado Valves, we’ve engineered hydraulic control components for nearly two decades. We serve mobile and industrial applications across India and export markets. This post explains what a pilot operated check valve does. It also explains why your choice of manufacturer matters more than most buyers realize.
What Is a Pilot Operated Check Valve?
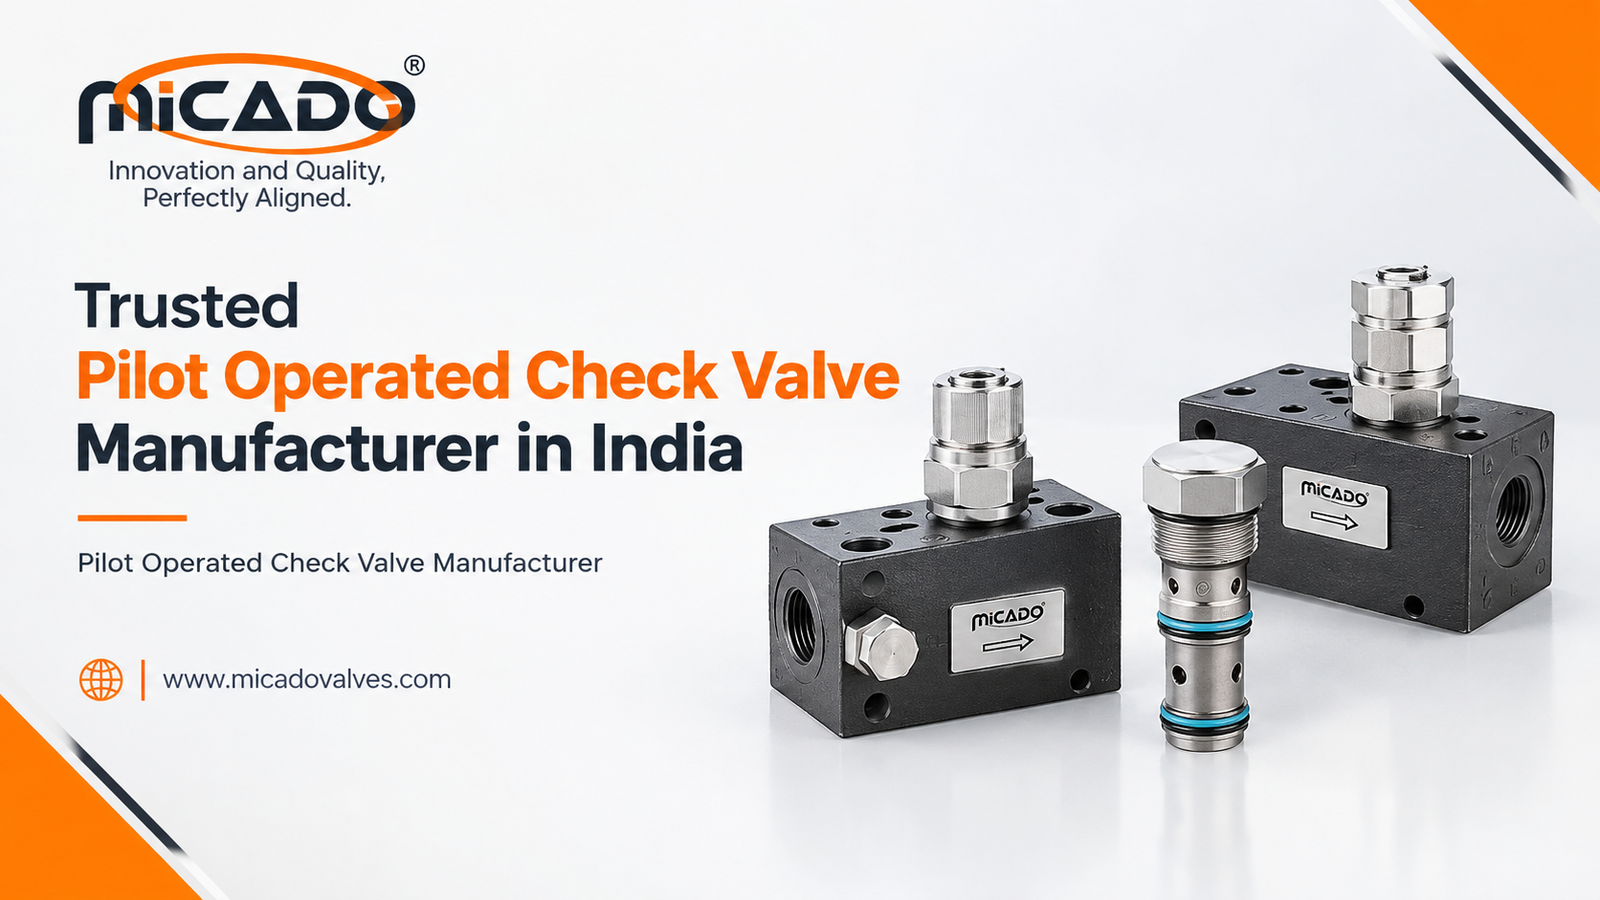
A standard check valve allows flow in one direction only. It blocks reverse flow. That’s useful, but limited. A pilot operated check valve adds a third port: the pilot line. Pilot pressure can force the valve open, even against reverse flow. This gives engineers precise control over when a circuit locks and when it releases.
Why the Pilot Mechanism Matters
Gravity and load pressure constantly try to move an actuator. This happens in lifting equipment, tippers, cranes, and mobile machinery. A pilot operated check valve stops the load from creeping or dropping. It holds firm even when the main control valve is centered, or when a hose fails upstream. This one component often stands between safe operation and serious accident.
Where These Valves Are Used
- Truck cranes and hydraulic lifting arms
- Tippers and dump-body mechanisms
- Agricultural machinery (loaders, implements)
- Construction and mining equipment
- Forklifts and material handling systems
A weak check valve tends to fail suddenly, and the failure is usually load-related. That makes manufacturing quality genuinely consequential.
Why the Choice of Manufacturer Matters
Not every valve stamped “pilot operated” performs the same way. Two valves can look identical on a datasheet. Under sustained pressure and years of duty cycles, they can behave very differently. This is where an established Pilot Operated Check Valve Manufacturer earns its reputation — through in-house engineering, tested tolerances, and real application experience.
Precision Manufacturing and Material Selection
Poppet geometry matters. Seat hardening matters. Spring calibration matters too. Together, these determine cracking pressure and leak-free holding. Micado valves are built to hold working pressures up to 250 bar. Our seats are hardened for long service life. They’re designed for consistent pressure holding, not just a good number on a factory test sheet.
Quality Control That Reflects Real Operating Conditions
A valve can pass every lab test and still fail in the field. Temperature swings, contamination, and vibration are constant real-world stresses. Manufacturing discipline is what closes that gap. Consistent tolerances, batch-level testing, and traceable materials separate a dependable Pilot Operated Check Valve Manufacturer from one competing on price alone.
What Sets Micado Valves Apart
Two Decades of Hydraulic Valve Engineering
Micado has specialized in hydraulic control valves since 2007. Our range covers monoblock and sectional directional control valves, hand-lever operated directional valves, pressure relief valves, and check valves — alongside our pilot operated check valve line. This breadth matters. A manufacturer who understands the full hydraulic circuit builds valves that integrate more predictably into a customer’s system.
Built for Indian Operating Conditions, Trusted Beyond
We operate out of Rajkot, Gujarat. Our valves are engineered for the conditions Indian agricultural, construction, and industrial equipment actually face: dust, heat, and demanding duty cycles. We also meet the expectations of export customers. Being a dependable Pilot Operated Check Valve Manufacturer in India means designing for these realities from day one. It’s not about adapting a generic global product later.
Application-Specific Customization
Every machine builder has different needs. Mounting, threading, and pressure requirements all vary. We don’t offer a rigid, one-size-fits-all catalog. Instead, we work directly with OEMs and equipment manufacturers. Together, we customize port sizing, cracking pressure, and pilot ratio to the actual application — whether that’s a truck crane, a tipper body, or an agricultural implement.
Key Technical Considerations When Selecting a Pilot Operated Check Valve
Cracking and Opening Pressure
This is the pressure at which the valve begins to open. It also includes the differential needed to fully open it. Both should match your system’s operating range precisely. A mismatch causes sluggish response. Or it causes premature opening under load.
Pilot Ratio
This determines how much pilot pressure is needed, relative to load pressure, to open the valve. Getting this ratio right is critical for load-holding applications. You need the valve to stay firmly closed until you deliberately release it.
Sealing and Leakage Tolerance
Even small leakage compounds over time in load-holding applications. This leads to drift. Hardened seats and tight manufacturing tolerances keep leakage within acceptable limits. This holds true across the valve’s full service life.
Why Partner With an Established Manufacturer
Sourcing decisions often come down to price per unit. But the real cost shows up later. It appears in field failures, warranty claims, and machine downtime. Working with a proven Pilot Operated Check Valve Manufacturer gives OEMs and end users real advantages:
- Consistent quality across production batches
- Technical support for application-specific selection
- A manufacturer who understands the full hydraulic circuit, not just one part
- Export-grade documentation and compliance where required
Conclusion
A pilot operated check valve may be a small part of a larger hydraulic system. But its role in safety and load control is disproportionately large. Choosing the right manufacturer matters. This protects your equipment. It protects your customers downstream too.
Micado Valves has built its reputation on these fundamentals: precision engineering, application-specific customization, and consistency you can rely on — shipment after shipment.
If you’re evaluating a Pilot Operated Check Valve Manufacturer for your next project, get in touch with our team to discuss specifications and application requirements.